CONSTROMECHTMEngineering Solution

Industries · Fertilizer & Chemical

Fertilizer & Chemical Processing PlantsChain Equipment Systems

Chain equipment for every stage of a fertilizer & chemical plant: what each machine does, the chain it runs on and the design data behind it — with the CONSTROMECH products that go into it.

4
Plant stages
11
Equipment systems
4
Chain types

Follow the material flow

Chain equipment, stage by stage

Plant zones in the order material moves through them. Each machine lists its duty, the chain it runs on and the design points we build to.

01

Raw Material Intake & Handling

4 equipment systems

At a glance · Raw Material Intake

Apron Weigh Feeders
Dust-tight systems for limestone, phosphate rock, granular materials.
Drag & Pan Conveyors
To move raw feed through crushers to reactors.

Apron Feeders (for Phosphate Rock, Urea, Potash, Limestone)

  • Purpose: Transfers mined or transported bulk material (e.g., phosphate rock, sulphur, ammonia nitrate) from hoppers/trucks to primary crushers or blending units.
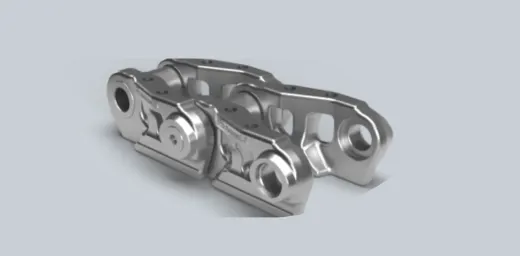
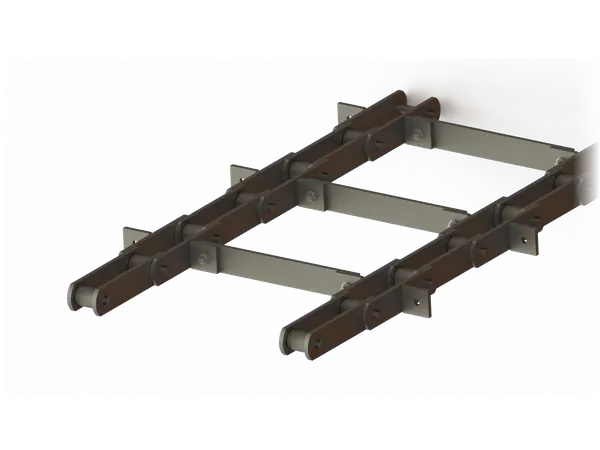
  • Chain Type: Drop-forged, or cast link chains; pitch ≥ 250 mm.

Features

  • Impact-resistant pans with alloy liners.
  • Throughput capacity: 200–1200 TPH.
  • Forged steel links with wear-resistant pins and bushings.

Reclaimers (Portal or Side Scraper)

  • Purpose: Extracts bulk material from stockpiles and feeds into process stream.
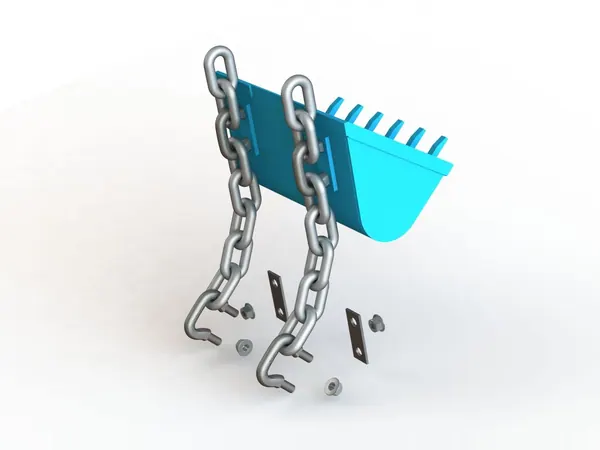
  • Chain Type: Round link or forged scraper chain.

Features

  • Equipped with variable-speed chain drive.
  • Built-in overload protection and synchronized travel drives.

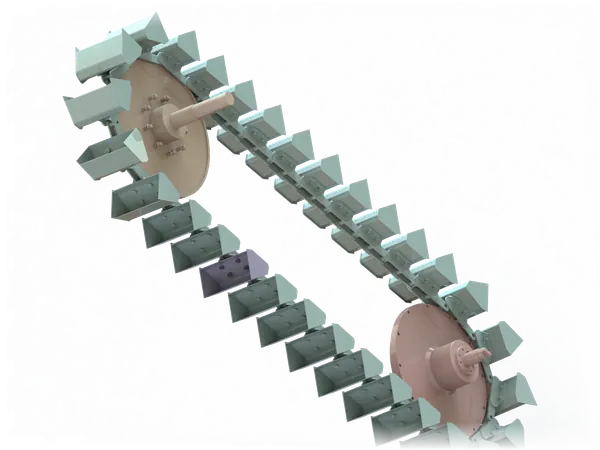
Chain Bucket Elevators

  • Purpose: Vertical lifting of ground raw mix, ammonia-based compounds, or intermediate products.
  • Chain Type: Central chain or round link DIN-type chain.

Elevator Features

  • Height: up to 60–80 m.
  • Capacity: 150–1000 TPH depending on material bulk density.
  • Heat resistance up to 250°C for exothermic products.

Drag Chain Conveyors (Blending Zone)

  • Purpose: Horizontal or inclined conveying between blenders, bins, granulators.
  • Chain Type: Drop-forged scraper or enclosed twin-strand drag chain.

Design Highlights

  • Wear-resistant flights with anti-corrosion coatings.
  • Dust-tight casings with multiple outlet provisions.

02

Granulation & Drying

2 equipment systems

At a glance

Bucket Elevators
Central-chain elevators for hot, damp granules into dryers or coolers.
Pan & Belt Conveyors
Beyond the dryer, for cooling and storage transfer.

Deep Pan Conveyors (for Granulated Products)

  • Purpose: Gentle, non-segregating transfer of granules to drying or cooling drums.
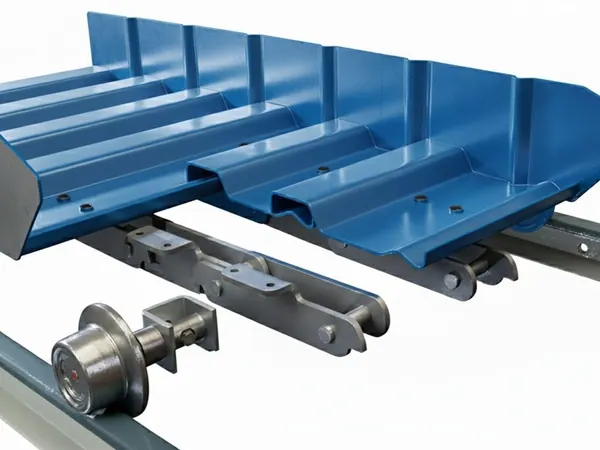
  • Chain Type: Central chain with deep-drawn pans.
  • Capacity: 300–600 TPH.
  • Temperature Resistance: Up to 300°C.
  • Notes: Controlled discharge prevents product degradation.

Cooling Zone Conveyors

Often use enclosed drag chain or multi-discharge chain conveyors to feed cooled product into silos or packing units.

03

Dust Handling & Gas Cleaning Units

1 equipment system

Flow Conveyors

  • Purpose: Ash, scrubber residue or filter dust conveying from ESP, baghouse or cyclones.
  • Chain Type: Forged scraper chain.

Features

  • Compact low-profile design.
  • Explosion-venting available as option.

04

Storage Silos & Batching

4 equipment systems

At a glance · Finished Product Handling & Bagging

Silo Discharge Systems
Weigh feeders, screw feeders, and apron feeders for precise dosing to bagging lines.
Belt Bucket Elevators
For final packaging feed at capacities ~300–800 m³/h.

Bucket Elevators (Packing Feeders)

  • Purpose: Elevate urea, DAP/NPK, or blended products into overhead silos.
  • Chain/Belt Type: Round link (for dusty or abrasive material) or belt-based for granular, low-abrasion use.

Special Notes

  • Optional belt/chain hybrids for reduced maintenance.
  • Self-cleaning return leg design.

Packing Elevators

  • Purpose: Feed material from silo to weighing/packing system.
  • Chain Type: Belt or compact central chain elevator.

Design Flexibility

  • Modular heights and compact headroom design.
  • Anti-bridging attachments for sticky urea or ammonium sulphate.

Truck/Wagon Loading Systems

Integrated with flow conveyors and telescopic spouts.

Optional chain-based discharge feeder to regulate flow into loader.

Common Chain Types & Technical Notes

Chain TypeApplication AreaDesign Notes
Forged Link ChainApron feeders, silo dischargeHeat-treated links with self-lubricating bushings
Round Link ChainBucket elevators, reclaimersDIN 764 / 22252 chains, suited for abrasive material
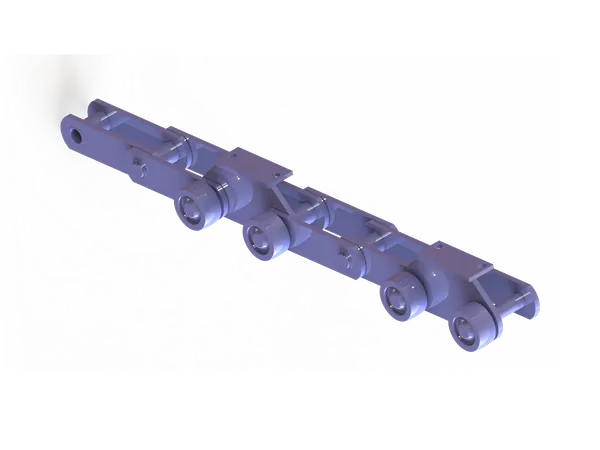
Central ChainPan conveyors, elevatorsAccurate pitch with wear-resistant forged links
Scraper ChainDrag/Flow conveyors, ESP ashDrop-forged scrapers, reversible drives
Chemical & Fertilizer Plant ServicesRetrofit, capacity enhancement, conversion and commissioning — zone by zone through your fertilizer & chemical plant.View services

CMECH Technical Services

How our field team supports fertilizer & chemical plants

Every engagement is carried out by our own field engineers — from the first inspection to commissioning and hand-over.

How we work
  • Site Inspections & Equipment Audits

    Bucket elevators, conveyors, ash systems, reclaimers

  • Installation & Commissioning Supervision

    Chains, buckets, bearings, drive units, structural supports

  • Corrective & Preventive Maintenance

    Hot/cold chain replacement, sprocket rebuilds, belt tracking

  • Retrofit & System Upgradation Projects

    Chain-to-belt elevator conversions, scraper design mods, capacity enhancements

  • Operational Optimization Support

    Root cause analysis, performance tuning, load balancing

Chains or spares for your fertilizer & chemical plant?

Send us your drawing or requirement — we respond within one business day.